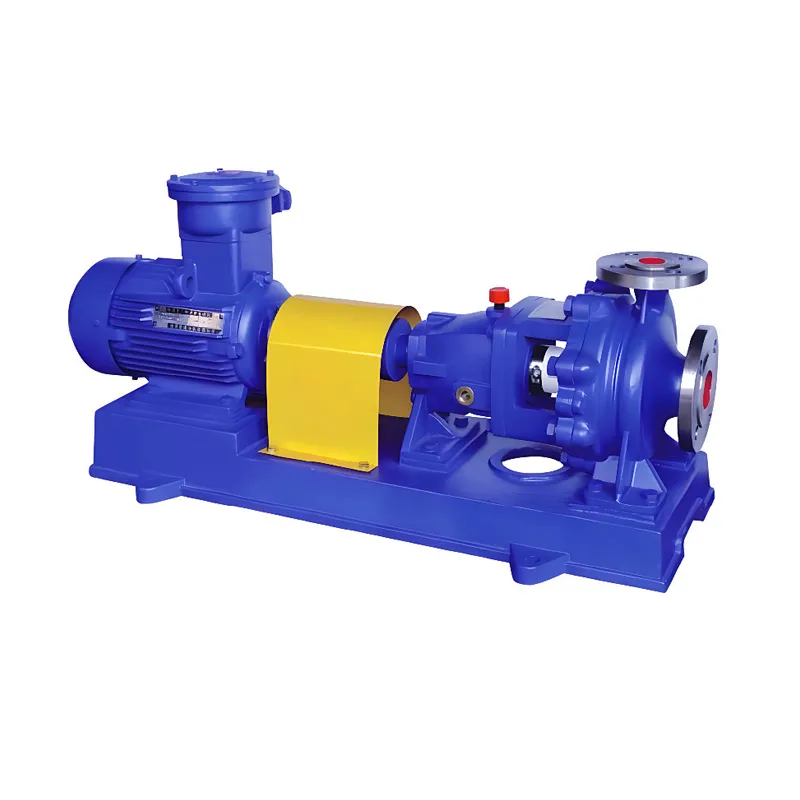
The IH chemical resistant transfer pump represents the pinnacle of reliability and efficiency in fluid handling for a wide range of industries. This horizontal, single-stage centrifugal pump is specifically engineered to manage everything from clear water to highly corrosive chemicals, acids, alkalis, solvents, and slurries without solid particles. Built in full compliance with international standards ISO 2858 and ISO 5199, it is the definitive solution for operators seeking superior performance, reduced lifetime costs, and unwavering dependability.
Key Features for IH corrosive liquid transfer pump
Advanced Hydraulic Design: Delivers optimized performance with 5% higher efficiency and a 2m lower NPSH requirement than legacy pumps, resulting in significant energy savings and greater operational flexibility.
Rear-Door Maintenance: Allows for complete access to the pump's rotating assembly without disconnecting the inlet or outlet pipelines. This innovative design drastically reduces service time and labor costs.
Compact & Lightweight Footprint: The direct motor coupling design (IH-A variant) minimizes space requirements and associated infrastructure expenses.
Enhanced Operational Integrity: An anti-vibration design featuring a steel wire screw sleeve secures the impeller nut against loosening, while reliable closed grease-lubricated bearings or automatic oil compensation systems ensure continuous, long-term operation.
Versatile Impeller Options: Available with close, semi-open, or open impellers to suit a diverse spectrum of fluid handling needs, including those with suspended solids.
Unmatched Reliability in Aggressive Environments
Constructed from premium corrosion-resistant materials such as 316L, 904, and Mo2Ti, the IH pump is built to withstand the most challenging operational conditions. Its robust design ensures long-term durability, minimizing downtime and maintenance costs in aggressive chemical processing environments.
Broad Application Versatility of IH chemical resistant centrifugal pump
The IH pump is ideally suited for transferring both corrosive and non-corrosive fluids across numerous sectors:
Chemicals & Petrochemicals: Acids, solvents, and hydrocarbons.
Energy & Utilities: Refineries, power stations, and seawater desalination plants.
Industrial Processes: Pharmaceutical manufacturing, paper and pulp production, and sugar refining.
Environmental Management: Wastewater treatment and centrifugal pump cooling system.
Marine & Offshore: Oil production and shipboard systems.
Technical Specifications of IH Chemical Process Pumps
The Global Standard for Efficiency
Officially endorsed by China's State Administration of Machinery as the preferred replacement for outdated and imported pumps, the IH series combines cutting-edge engineering with global standards compliance. With its proven corrosion resistance, modular design, and low-maintenance operation, it offers a cost-effective and high-performance solution for your most critical fluid transfer challenges.
Why Choose IH small chemical pump?
For unmatched performance in refineries, desalination plants, and chemical processing facilities worldwide, trust IH Pumps to deliver operational versatility and enduring reliability.
Custom configurations are available to meet specialized requirements.
We can also provide kinds of centrifugal pump china for sale, if you are interested, please contact us.